Pre-Install Checklist: Verifying Racking Coatings
This checklist helps you verify the coating and material integrity of racking before installation. It covers surface inspection, material confirmation, and documentation checks to catch defects early and prevent corrosion issues during the project lifecycle.
- Check for coating defects like pinholes, blisters, or rust spots before unloading materials
- Verify material specs match the purchase order, including alloy type and coating thickness
- Review mill certificates and coating test reports as part of your documentation checklist
- Use proper lighting and magnification to detect subtle surface issues that are easy to miss
- Document all findings and resolve discrepancies with the supplier before installation begins
Why Coating Integrity Matters Before Installation
Coated racking gets its protection from the coating, not the base metal alone. If the coating is damaged or incomplete, the underlying material will corrode when exposed to moisture, salt air, or temperature cycling. A defect that looks minor on the warehouse floor can become a structural issue years later.
The pre-installation inspection is your last chance to catch problems before the racking goes up. Once the structure is on site and covered by solar panels, you cannot easily inspect the fasteners, welds, or coating edges. Finding a problem now costs hours. Finding it after installation costs days and potential downtime.
This checklist is structured to help your team verify coating and material integrity systematically. It works for steel, aluminum, and composite racking systems, though the specific checks vary by material. Read through the sections in order, or print them out and use them as a field guide.
Surface Inspection: What to Look For on the Coating
Start with a visual sweep of every component. Lay the parts out on a clean, dry surface. Use a flashlight at a low angle to catch texture changes that a straight-on view misses.
Look for these specific defects:
- Pinholes and porous areas. These are tiny openings where the base metal shows through. They often form during the coating process when gas bubbles escape unevenly. On steel, pinholes are the start point for rust.
- Blisters and bubbles. These indicate the coating was applied over moisture or contamination. The coating may peel away over time, exposing the metal.
- Rust or oxidation spots. Even if the base material is supposed to be stainless or aluminum, surface rust indicates contamination or improper handling. On steel, any red-brown discoloration is a red flag.
- Scratches and abrasions. Deep scratches that expose the base metal are the most common issue. Check around bolt holes, welds, and cut edges.
- Coating thickness variations. Some areas may look thin or patchy. If you have a coating thickness gauge, measure several points on each component type.
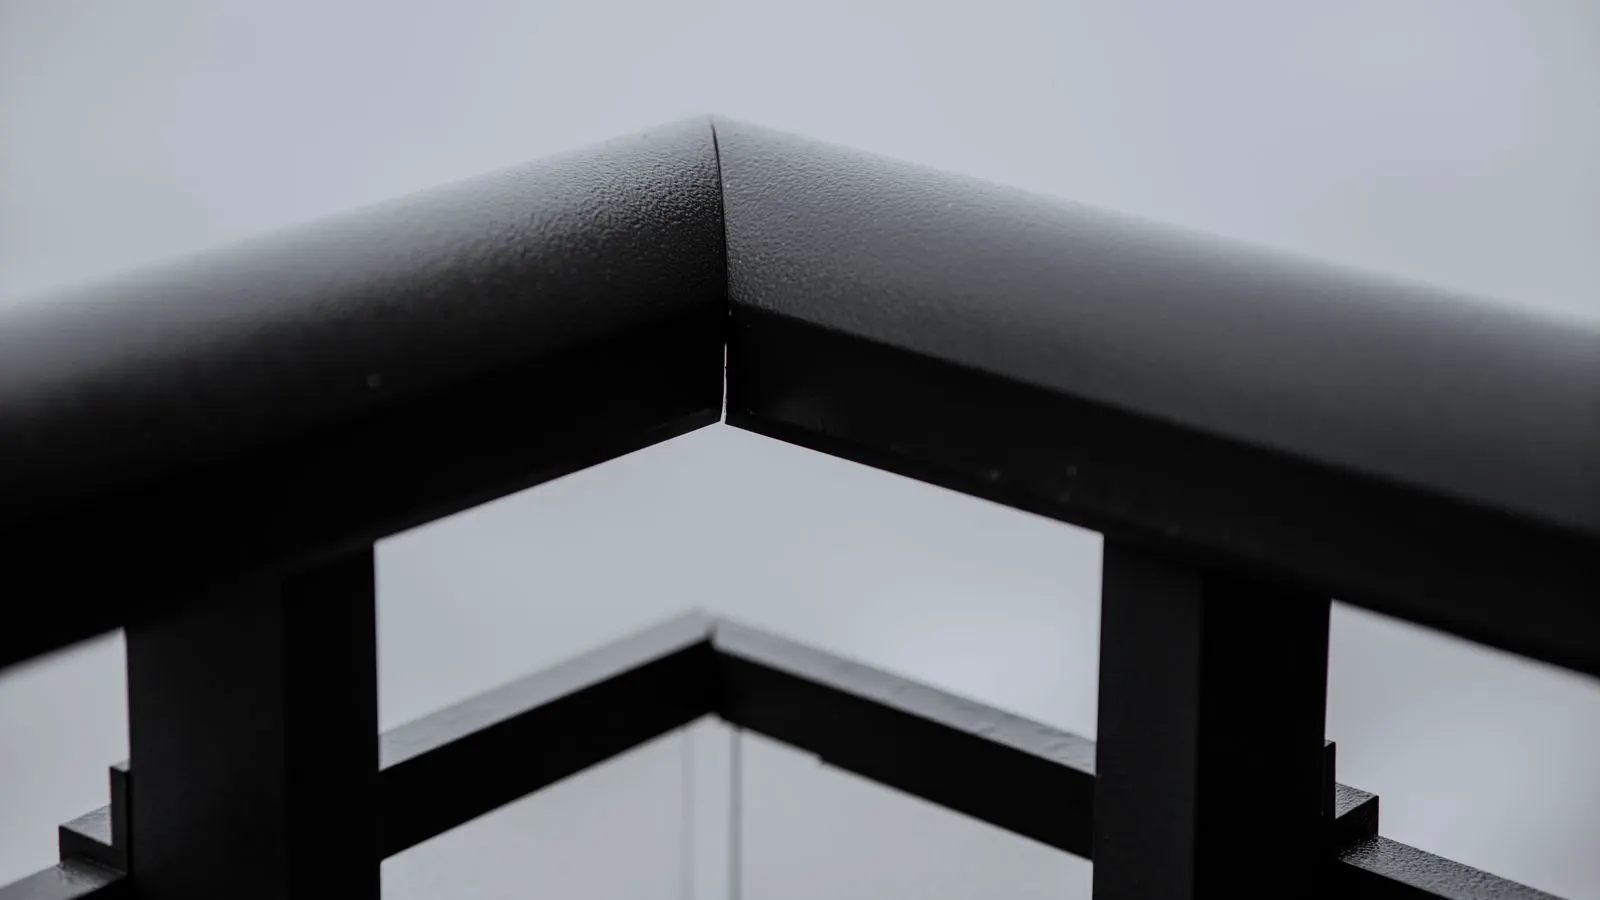
- Edge damage. Cut edges and drilled holes often have less coating than flat surfaces. These are high-risk areas for corrosion.
Red flags: If you see more than a few pinholes per component, or if the coating appears to be peeling or flaking, reject the batch. A supplier should be able to explain the cause and provide replacement or repair. Do not assume that a light scratch will not matter. On coastal or industrial sites, even minor exposure accelerates corrosion.
Material Verification: Confirming What You Actually Received
The coating is only one part of the story. You need to verify that the base material matches what you specified. A supplier might ship a lower-grade steel to save cost, or a different aluminum alloy than expected.
Check these items:
- Alloy designation. For steel, verify the grade (for example, standard carbon steel versus high-strength low-alloy steel). For aluminum, confirm the alloy series.
- Mill or heat certificates. These documents show the chemical composition and mechanical properties of the batch. Match them to the heat numbers stamped on the components.
- Coating specification. For galvanized steel, verify the coating weight or thickness. For painted or powder-coated systems, check the coating type, thickness, and finish.
- Fastener compatibility. If the fasteners are part of the package, verify their material. Mixing incompatible metals can cause galvanic corrosion.
Red flags: If the mill certificates are missing, incomplete, or do not match the heat numbers on the parts, stop. Do not install until the documentation is resolved. If the components look different from previous batches, even if the paperwork says they are the same, ask questions.
Documentation and Traceability Checklist
Paperwork is not optional. It is your legal and technical record of what was delivered. Without it, you cannot prove that the material met the specification at the time of delivery.
Gather and verify:
- Purchase order or contract. Confirm the material specifications match what was ordered.
- Material test reports. These should include tensile strength, yield strength, and coating thickness data.
- Coating inspection reports. For powder-coated or painted systems, these may include adhesion test results.
- Certificate of conformity. A signed document from the supplier confirming the batch meets the specified standards.
- Chain of custody records. If the racking was stored for a long time or changed hands, verify that the storage conditions were appropriate.
Red flags: Generic documents without specific batch numbers, missing signatures, or reports that do not reference the exact part numbers. If the supplier cannot provide the mill certificates within a reasonable timeframe, treat it as a quality concern.
Storage and Handling Check Before Unloading
Coating damage often happens between the factory and your site. The racking may have been fine when it left the supplier, but damage can occur during transport or temporary storage.
Check these conditions:
- Packaging integrity. Are the components wrapped in protective film or foam? Is the packaging torn, wet, or crushed?
- Stacking method. Are heavy components placed on top of lighter ones? Are components stacked so that they do not press against each other at the coating edges?
- Environmental exposure. If the racking was stored outdoors, check for rain exposure, UV fading, or condensation. If it was stored in a container, check for moisture.
- Handling marks. Look for dents, bends, or deformation. Even if the coating is intact, a bent component may not meet structural specifications.
Red flags: If the packaging is damaged and the components show corresponding marks, inspect every part in that batch. If the racking was stored in a damp environment, check for condensation inside the packaging. This can cause early corrosion on the base metal.
Fastener and Connector Inspection
The racking structure is only as good as its connections. Fasteners, clamps, and connectors are high-stress points, and their coatings are often thinner or less durable than the main structural members.
Inspect:
- Fastener coating. Do the bolts, nuts, and washers have a consistent coating? Are there bare metal areas?
- Thread condition. Check the threads for damage or corrosion. A damaged thread can strip under load.
- Compatibility. If you are mixing fasteners from different suppliers or batches, verify that the materials are compatible.
- Quantity count. Verify that the fastener count matches the bill of materials. Missing fasteners will be obvious once the racking is up.
Red flags: If the fasteners are coated in a color or finish that differs from the structural members, ask the supplier about the coating specification. If the fasteners show any signs of rust or pitting, reject them. Fastener corrosion is one of the most common early failure points in racking systems.
Final Review and Sign-Off
Before the racking goes up, take a step back and review the entire inspection process.
- Summarize findings. List any defects, discrepancies, or documentation gaps.
- Classify issues. Separate critical issues (structural damage, major coating failure, missing mill certificates) from minor issues (small scratches, cosmetic defects).
- Resolve or reject. For critical issues, stop installation and require supplier action. For minor issues, agree on a plan with the supplier and document the resolution.
- Sign off. Have a project manager or engineer sign the inspection report. This creates a clear record that the material was verified before installation.
Red flags: Pressure to install despite unresolved issues. If the supplier or contractor is pushing to start installation before the inspection is complete, pause. The time it takes to resolve a documentation or coating issue is small compared to the cost of a corrosion failure after installation.
Quick Reference Table: Coating Defect Types and Responses
| Defect Type | Typical Cause | Risk Level | Recommended Action |
|---|---|---|---|
| Pinholes | Gas escape during coating | Medium | Measure density; replace if high |
| Blisters | Moisture or contamination | High | Reject affected batch |
| Deep scratches | Handling or transport | Medium | Assess depth; replace if base metal exposed |
| Rust spots | Contamination or storage | High | Reject and require replacement |
| Thin coating | Application error | Medium | Measure thickness; replace if below spec |
| Edge damage | Cutting or drilling | Medium | Check high-stress areas; repair if needed |
Use this table as a quick reference during your inspection. If a defect type is not listed, document it and consult the supplier. Do not guess.
Frequently asked questions
How often should I inspect coated racking after installation?
Check the racking during routine site maintenance, at least once per year. Focus on fasteners, welds, and areas where the coating may have been damaged during installation.
Can I install racking with minor coating scratches?
It depends on the location and severity. On mild environments, small scratches may be acceptable. On coastal or industrial sites, even minor scratches can lead to corrosion. When in doubt, reject the part.
What if the mill certificates do not match the heat numbers?
Stop the installation and contact the supplier. Do not proceed until the documentation is resolved. A mismatch can indicate a wrong batch or a documentation error.
Do composite racking systems need the same coating inspection?
Composite systems do not have a metallic coating in the same way. Focus on surface integrity, UV damage, and structural integrity instead. Check for cracks, delamination, or exposure of the core material.
How do I measure coating thickness?
Use a calibrated coating thickness gauge. Take multiple readings on each component type and average the results. Compare the readings to the specified minimum thickness.